On Site Machining of a David Brown Gearbox
Overview
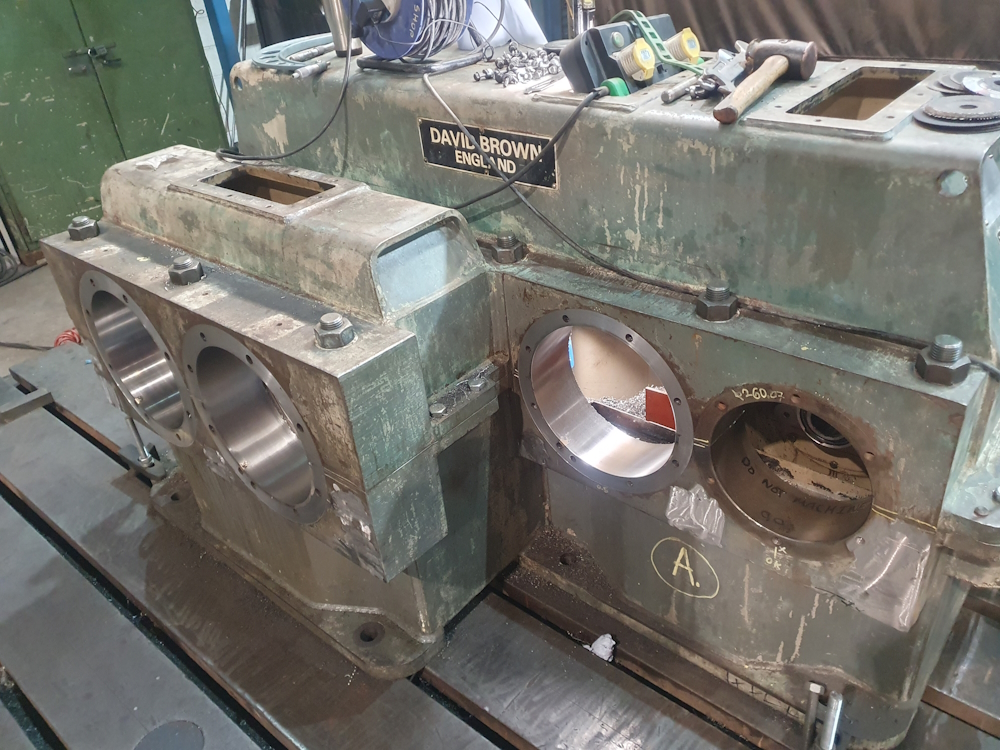
Benroc Engineering was contracted to complete critical machining on a David Brown gearbox after a previous supplier failed to deliver. The gearbox had already undergone weld reclamation on several bores, but the machining stage—required to return the component to OEM specification—remained incomplete. Our team mobilised quickly to recover the project and ensure full dimensional accuracy.
Challenge
The seven bearing bores needed machining in the correct position, size, and tolerance. Before this could be achieved, the gearbox’s split line contained excessive weld material, preventing the two halves from clamping together accurately.
Our Approach
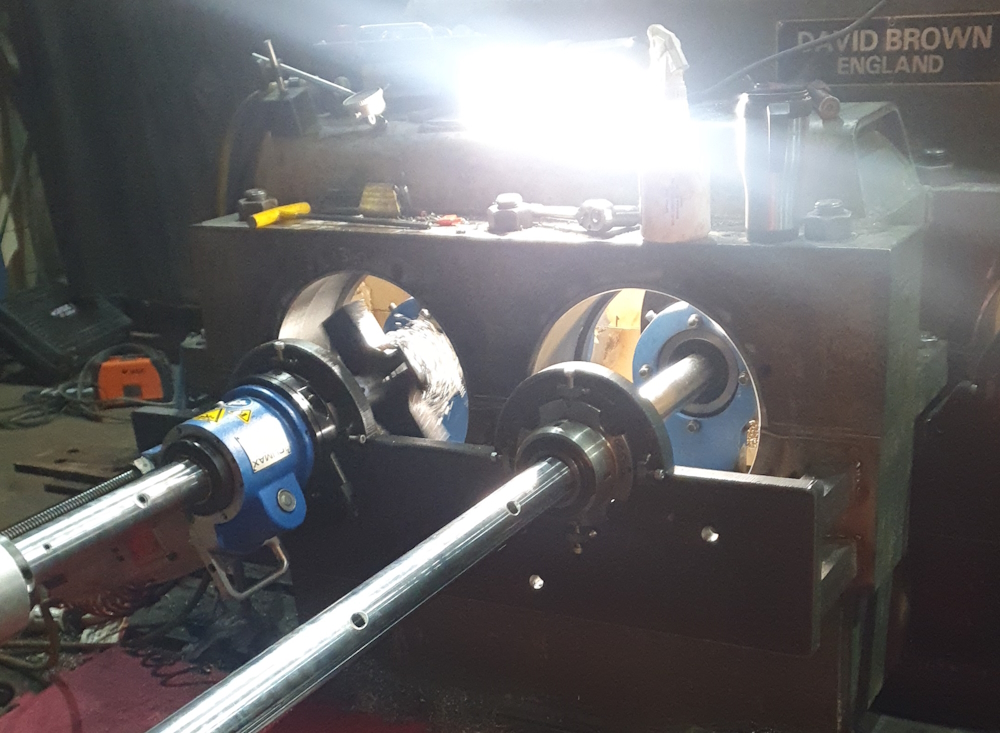
Benroc Engineering deployed an on‑site machining team equipped with multi‑bar boring systems. The project involved several key stages:
- Split‑line preparation: Machining away excess weld to allow precise clamping and alignment of the gearbox halves.
- Multi‑bar setup: Installing four boring bars across the assembled gearbox to ensure all bore positions were controlled and machined relative to each other.
- Alignment and levelling: Using multiple methods to set the boring bars level, correctly pitched, and aligned to the gearbox’s original centreline.
- Precision machining: Re‑boring all seven weld‑repaired bores to final size and machining the associated faces to accept gearbox caps.
Our approach ensured concentricity, correct pitch, and accurate alignment across all bores.
Results
Post‑machining verification showed restored concentricity and alignment. Gear bluing validation confirmed accurate tooth contact patterns. The gearbox achieved full operational readiness with all geometries restored to specification.
What this Demonstrates
This highlights Benroc Engineering’s ability to step in, solve complex machining challenges, and deliver dependable results when precision matters most.